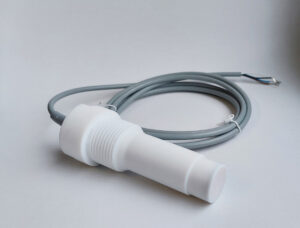
The capacitive food sensor is the ideal solution for detecting the level and presence of liquids and solids in food & beverage sector systems.
Designed to ensure maximum safety, precision and reliability, this food grade level sensor is designed for applications where hygiene, regulatory compliance and chemical resistance represent fundamental requirements for production continuity.
Made with MOCA certified Teflon PTFE case, the device ensures full suitability for direct contact with food. It complies with EC 1935/2004, EC 10/2011, EC 2023/2006 (GMP) and FDA CFR 21 177.1550 regulations, ensuring compliance with European and international food safety standards. This makes it particularly suitable as a component for food systems intended for the transformation, processing, storage and packaging of food products.
The surface with a minimum roughness of 2.4 µm reduces the risk of accumulation of residues and bacterial contamination, facilitating cleaning operations and contributing to the maintenance of high hygiene standards. This feature is essential in processes where the quality of the final product depends on the rigorous control of operating conditions.
The 1″ threaded connection allows for simple and quick installation on tanks, hoppers, silos and pipes, ensuring reliable integration into existing systems and reducing machine downtime. Thanks to capacitive technology, the sensor precisely detects granular materials, powders, liquids and viscous substances, improving process control, inventory management and operational efficiency.
Robust, compact and highly performing, the capacitive sensor for food use represents a strategic choice for companies that wish to optimize safety, quality, traceability and production continuity in compliance with current regulations.
Data Sheet: Sm-cp023-cp10-d25-5g1-a-k-ptfe-l110